Rigid Box Materials Guide: How to Choose Board, Paper, Fabric and Inserts
Most rigid boxes combine a 1–3 mm greyboard or chipboard core with an outer wrap of printed paper, specialty paper or book cloth, plus an inner lining and, when needed, a protective insert. There is no single best combination. The right materials depend on the product weight, box size, required appearance, opening structure, protection level and expected handling.
A small perfume box may use dense board, smooth printed paper and a precisely cut insert. A wine box usually needs greater panel stiffness and a load-bearing support. A foldable presentation box needs dimensionally stable board panels and a covering material that can bend repeatedly at the joints. Choose for the finished box first, then confirm that the complete material structure can be produced consistently.
Quick material selection
Core: greyboard or another dense paperboard provides the box shape and stiffness.
Outer wrap: printed paper, specialty paper, kraft paper or book cloth creates the visible finish.
Inner lining: paper or cloth covers exposed board and completes the interior.
Insert: paperboard, molded pulp, foam, EVA or a fabric-covered support holds and protects the product.
What Materials Are Used to Make Rigid Boxes?
A conventional rigid box has a solid paperboard structure rather than a corrugated fluted core. Greyboard is widely used because it combines stiffness, density and clean cutting performance. Depending on the supplier and market, similar grades may be described as chipboard, recycled board, kraft chipboard or binder’s board.
The board is normally hidden beneath a decorative covering. Coated art paper supports detailed printing; uncoated and kraft papers create a natural look; textured, metallic, pearlescent and dyed-through papers add tactile or visual effects; and book cloth or paper-backed fabric produces a textile finish.
Inside the box, a lining covers the exposed board. An insert may then be added to locate the product. These layers have different jobs: the board controls structure, the wrap controls appearance and surface durability, and the lining or insert controls presentation, fit and protection.
Which Rigid Box Materials Are Best for Different Products?
Material selection should begin with what the finished package must do. Product weight, fragility, brand positioning, shipping conditions and opening experience are more useful starting points than choosing a fashionable paper and building the box around it.
Cosmetics, Perfume and Jewelry
These products usually benefit from dense, smooth board that produces straight edges and consistent gaps. Printed coated paper works well for detailed graphics, while embossed paper, soft-touch finishes, book cloth and paper-backed fabric can create a more tactile premium surface. EVA, foam, paperboard or fabric-covered inserts are common when the product must remain precisely positioned.
Wine and Spirits
Bottle packaging must support more weight and resist distortion during lifting and transport. A stiffer board, reinforced structure and durable covering are usually more important than an unusually elaborate surface finish. The insert should control bottle movement and spread the load without pushing the tray or lid out of shape.
Electronics and Mobile Devices
Electronics boxes typically need a clean surface, accurate fit and protection against impact and abrasion. Dense board and a scuff-resistant paper or laminated wrap are common choices. Engineered paperboard, molded pulp, foam and EVA provide different balances of cushioning, appearance, recyclability and cost.
Cigarettes and Premium Consumer Goods
Narrow printed borders and repeated graphic alignment make dimensional consistency especially important. Flat covering paper, stable board, accurate sheet cutting and predictable coating behavior usually matter more than maximum board thickness. Variation in paper stretch or board size becomes visible when the design uses fine borders and tight gaps.
Tea, Food and Gift Sets
Kraft paper, printed paper, specialty paper and cloth can all support different brand styles. For food and tea, odor, moisture exposure and migration requirements also matter. A decorative rigid box should not automatically be treated as suitable for direct food contact; an appropriate primary package or certified inner barrier may still be required.
Foldable and Book-Style Boxes
These structures use several board panels separated by joints or hinge spaces. The board must remain dimensionally stable, while the outer wrap and lining need enough flexibility to bend without cracking, lifting or creating excessive springback. Panel spacing, grain direction and adhesive performance are critical to smooth opening and flat closing.
What Is the Difference Between Greyboard and Chipboard?
Greyboard usually refers to a dense recycled paperboard with a grey appearance throughout the sheet. Chipboard is a broader term that can describe several grades of non-corrugated paperboard, and its meaning varies between suppliers and markets.
Greyboard is the standard structural core for many premium rigid boxes because it provides stiffness and can be cut or grooved accurately. Kraft chipboard has a brown appearance and may suit a natural packaging concept. Duplex or coated chipboard has a smoother face and is useful when part of the board remains visible or requires a cleaner surface.
“Chipboard” alone is not a complete specification. It can even be confused with wood particleboard, which is not a conventional rigid box material. A purchasing specification should identify the exact board grade, nominal thickness, thickness tolerance, density, stiffness, sheet size, squareness, moisture, flatness and surface cleanliness.
Two boards that both measure 2 mm can produce very different results. A dense board may retain a sharp edge and resist crushing, while a softer grade may compress at the corners or bow across a large panel. Thickness is important, but it does not replace density and stiffness data.
What Thickness of Greyboard Is Used for Rigid Boxes?
Greyboard around 1–3 mm thick is common in rigid box production, but the correct thickness must be chosen for the finished box. Small jewelry or cosmetic boxes may use a lighter structure, while a large wine or presentation box may need thicker, denser or reinforced board.
Increasing thickness can improve rigidity, but it also increases box weight, corner buildup and the space needed at hinges and panel gaps. It changes both the internal and external dimensions, so the insert, lid clearance and product fit must be recalculated rather than copied from a thinner-board design.
Choose board thickness together with:
- Box dimensions: large panels need enough stiffness to resist bowing.
- Product weight: heavy products may need reinforced panels or supports as well as thicker board.
- Box structure: lid-and-base, drawer, book-style and foldable boxes load the board differently.
- Edge design: thicker board requires sufficient turn-in and clean corner construction.
- Material grade: density and bending stiffness can make one 2 mm board perform differently from another.
A machine’s published board range is a processing limit for a particular configuration, not a recommendation for package design. The box requirement should determine the starting specification.
What Is the Best Paper for Rigid Box Wrapping?
There is no universal best wrapping paper. Coated art paper is a practical choice for high-resolution printing; uncoated or kraft paper suits a natural look; specialty paper adds texture, color or reflective effects; and laminated paper improves surface resistance. The best option is the one that creates the required appearance while folding, gluing and wearing acceptably.
Coated art paper gives a smooth surface for photographs, fine text and accurate brand colors. Uncoated and kraft papers feel more natural and usually absorb water-based adhesive more readily, although absorption rate varies by grade. Dyed-through paper can reduce the visibility of white edges. Embossed and textured papers add tactility but can make fine printing and sharp corner wrapping more demanding.
Pearlescent, metallic, foil-covered, laminated and heavily varnished papers can provide strong visual effects and better surface protection. Their closed or reflective surfaces may absorb less adhesive, show fold whitening or require different positioning marks. The finished decorated sheet—not only the unprinted base paper—should therefore be approved.
Do not choose wrapping paper by gsm alone
Papers with the same grammage can have different caliper, stiffness, grain, coating, friction and fold memory. One may form clean corners, while another cracks, springs back or shifts after positioning.
Can All Rigid Box Materials Be Used on Automatic Machines?
No. A material can be suitable for the finished package but still need a different process, setting or machine configuration. Flatness, stiffness, static, friction and sheet separation affect feeding. Coatings and surface energy affect adhesive bonding. Grain, thickness and elastic recovery affect folding, while reflective or low-contrast surfaces can affect registration detection.
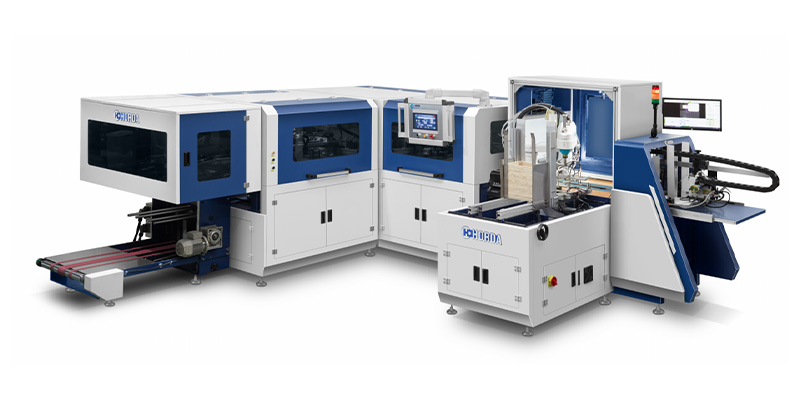
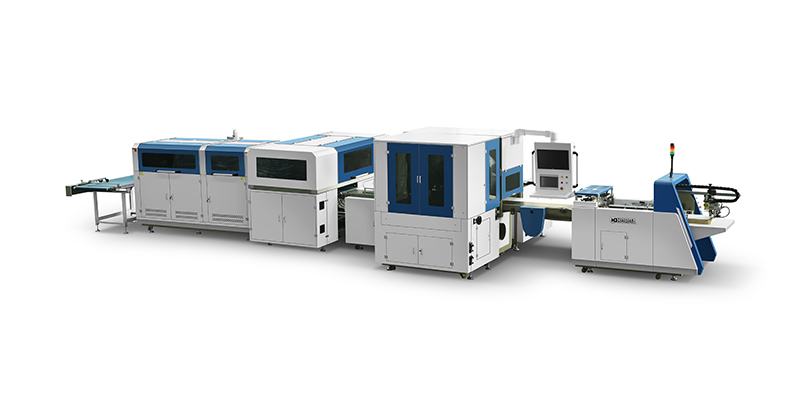
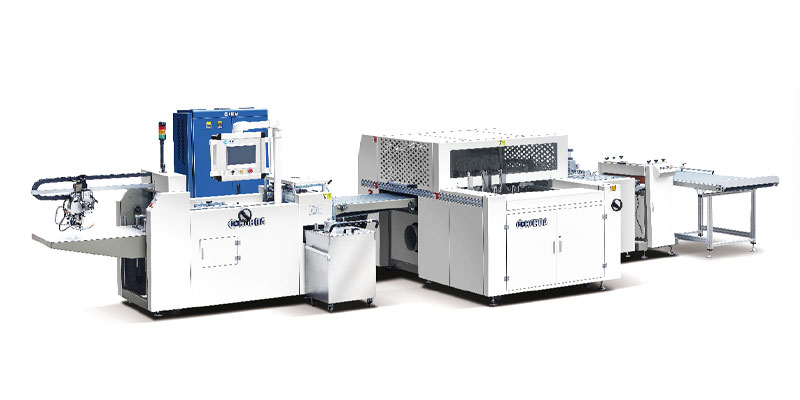
Different rigid box making machines cover different working sizes, board structures, positioning methods and folding processes. A multi-panel foldable design may instead require dedicated foldable rigid box equipment that controls panel spacing, wings and hinge areas. The material range of one model should never be applied to every machine or every stage of production.
When checking compatibility, provide the finished production material rather than only its name and thickness. Record board density and flatness, paper gsm and caliper, grain direction, backing, coating, lamination, embossing and actual sheet size. A 2 mm board with warped or dusty sheets may feed less reliably than a thicker but flatter and cleaner grade.
Can Fabric Be Used to Cover Rigid Boxes?
Yes. Book cloth and paper-backed fabric are widely used for presentation boxes, jewelry boxes, book-style cases and other premium packaging. The backing makes the material more dimensionally stable, creates a uniform gluing surface and reduces fraying, so it is generally easier to process than unsupported textile.
Linen-like cloth creates a visible weave and traditional bookbinding appearance. Velvet and suede-effect materials provide a soft finish but may show pressure marks or directional shading. Synthetic cloth and faux leather can improve durability and moisture resistance, although their surface energy and elasticity may require a different adhesive.
Before approving a fabric, check stretch in both directions, fraying, lint, adhesive penetration, visible staining, corner buildup, pressure marking and dimensional change after drying. A cloth that looks good on one handmade sample may stretch or skew during repeat production.
What Materials Are Used for Rigid Box Inserts?
An inner lining and an insert are not the same thing. The lining covers exposed board and finishes the interior surface. The insert locates, supports or cushions the product.
- Paperboard partitions: useful for lightweight products, sets and paper-based packaging concepts.
- Molded pulp: provides shaped support and a fiber-based option for electronics, cosmetics and gift products.
- EVA: produces precise cutouts and a clean presentation for cosmetics, electronics, tools and accessories.
- Foam: provides cushioning for fragile products, with performance depending on density and recovery.
- Fabric-covered inserts: add a premium finish but require careful control of wrinkles, adhesive, edge finishing and fitted dimensions.
The right insert depends on product weight, fragility, shape, removal force, presentation and sustainability targets. It must leave enough clearance for the product and closure. An oversized or overly stiff insert can distort the tray, stop the lid from closing or affect a book-style hinge. Odor, abrasion, color transfer and long-term compression should also be checked for sensitive products.
Why Do Rigid Boxes Warp, and How Can You Prevent It?
Rigid boxes commonly warp when the board, outer wrap and inner lining expand, contract or dry at different rates. Uneven moisture, curled sheets, opposing grain directions, unbalanced material thickness and inconsistent adhesive application can all pull a panel out of shape.
Start with flat board and covering sheets. Warped board can remain visible beneath the wrap, especially on large lids and cases, while curled paper can create uneven tension, bubbles or lifted edges. Store materials flat, protect them from rapid environmental changes and allow them to acclimate before production.
Grain direction also matters. Paper and board bend and move differently with and across the fiber direction. In book-style cases, grain is commonly arranged parallel to the spine or principal hinge to support smoother opening. The correct direction for other structures should be confirmed with a sample rather than copied as a universal rule.
Balance the two sides of a broad panel wherever possible. A heavily coated outer wrap paired with a very different inner lining can create unequal tension as the adhesive dries. Consistent glue application, suitable pressing and sufficient stabilization time help reveal whether the completed structure will remain flat.
How Do You Test Rigid Box Materials Before Mass Production?
Test the complete decorated material set: actual board, printed or finished wrap, lining, adhesive and insert. Printing, lamination, varnish, foil, embossing and fabric backing can change the way a material feeds, bonds and folds.
- Define the finished box. Record its structure, dimensions, product weight, appearance standard, closure and insert.
- Document each material. Include board grade, thickness and density; paper gsm and caliper; grain direction; coating; backing; and surface finish.
- Inspect incoming sheets. Check thickness variation, size, squareness, flatness, color, dust and cut-edge quality.
- Run the actual format. Test feeding and positioning with the intended sheet size, print design and finish at a representative production speed.
- Check adhesive performance. Observe glue coverage, open time, sliding, bleed-through, drying and final bond strength.
- Inspect folds and corners. Look for cracking, whitening, springback, thick buildup, wrinkles and exposed board.
- Measure the completed box. Verify dimensions, flatness, lid or drawer fit, hinge action and closing alignment after stabilization.
- Use a representative run. A few perfect samples do not reveal feeding variation, gradual curl or differences across a batch.
If multiple suppliers, colors or finishes will be used, test the combinations most likely to be difficult rather than approving only the easiest material. Keep approved samples and material specifications together so later batches can be compared with the same standard.